Advancing medicines
that matter.
From the first preclinical batch to commercial launch and beyond, Resilience keeps your biologics and sterile drug product programs moving toward the patients who need them.
Built on Experience.
Focused on What's Next.
Resilience is the CDMO partner for biotech and pharma companies at every stage of development and manufacturing.
Our teams bring more than 20 years of expertise across biologics drug substance and sterile drug product, with device assembly, labeling, and packaging capabilities that extend through market-ready finished goods. Across our North American network, experienced teams, advanced technology, and proven manufacturing operations turn promising science into dependable supply. And from day one, we plan for what comes next, giving every program the best chance to become a medicine that matters.
Resilience and Lilly Invest $750 Million to Increase US-Manufactured Medicine Supply
Resilience and Lilly are expanding a partnership that began in 2023. A new $750 million investment grows our Ohio operations and adds KwikPen® device manufacturing.
Capabilities for Clinical and Commercial Programs
Start at any phase of your program. Choose drug substance, drug product, or both, whether that means beginning with development and tech transfer, scaling up later, or bringing us material you've already made.
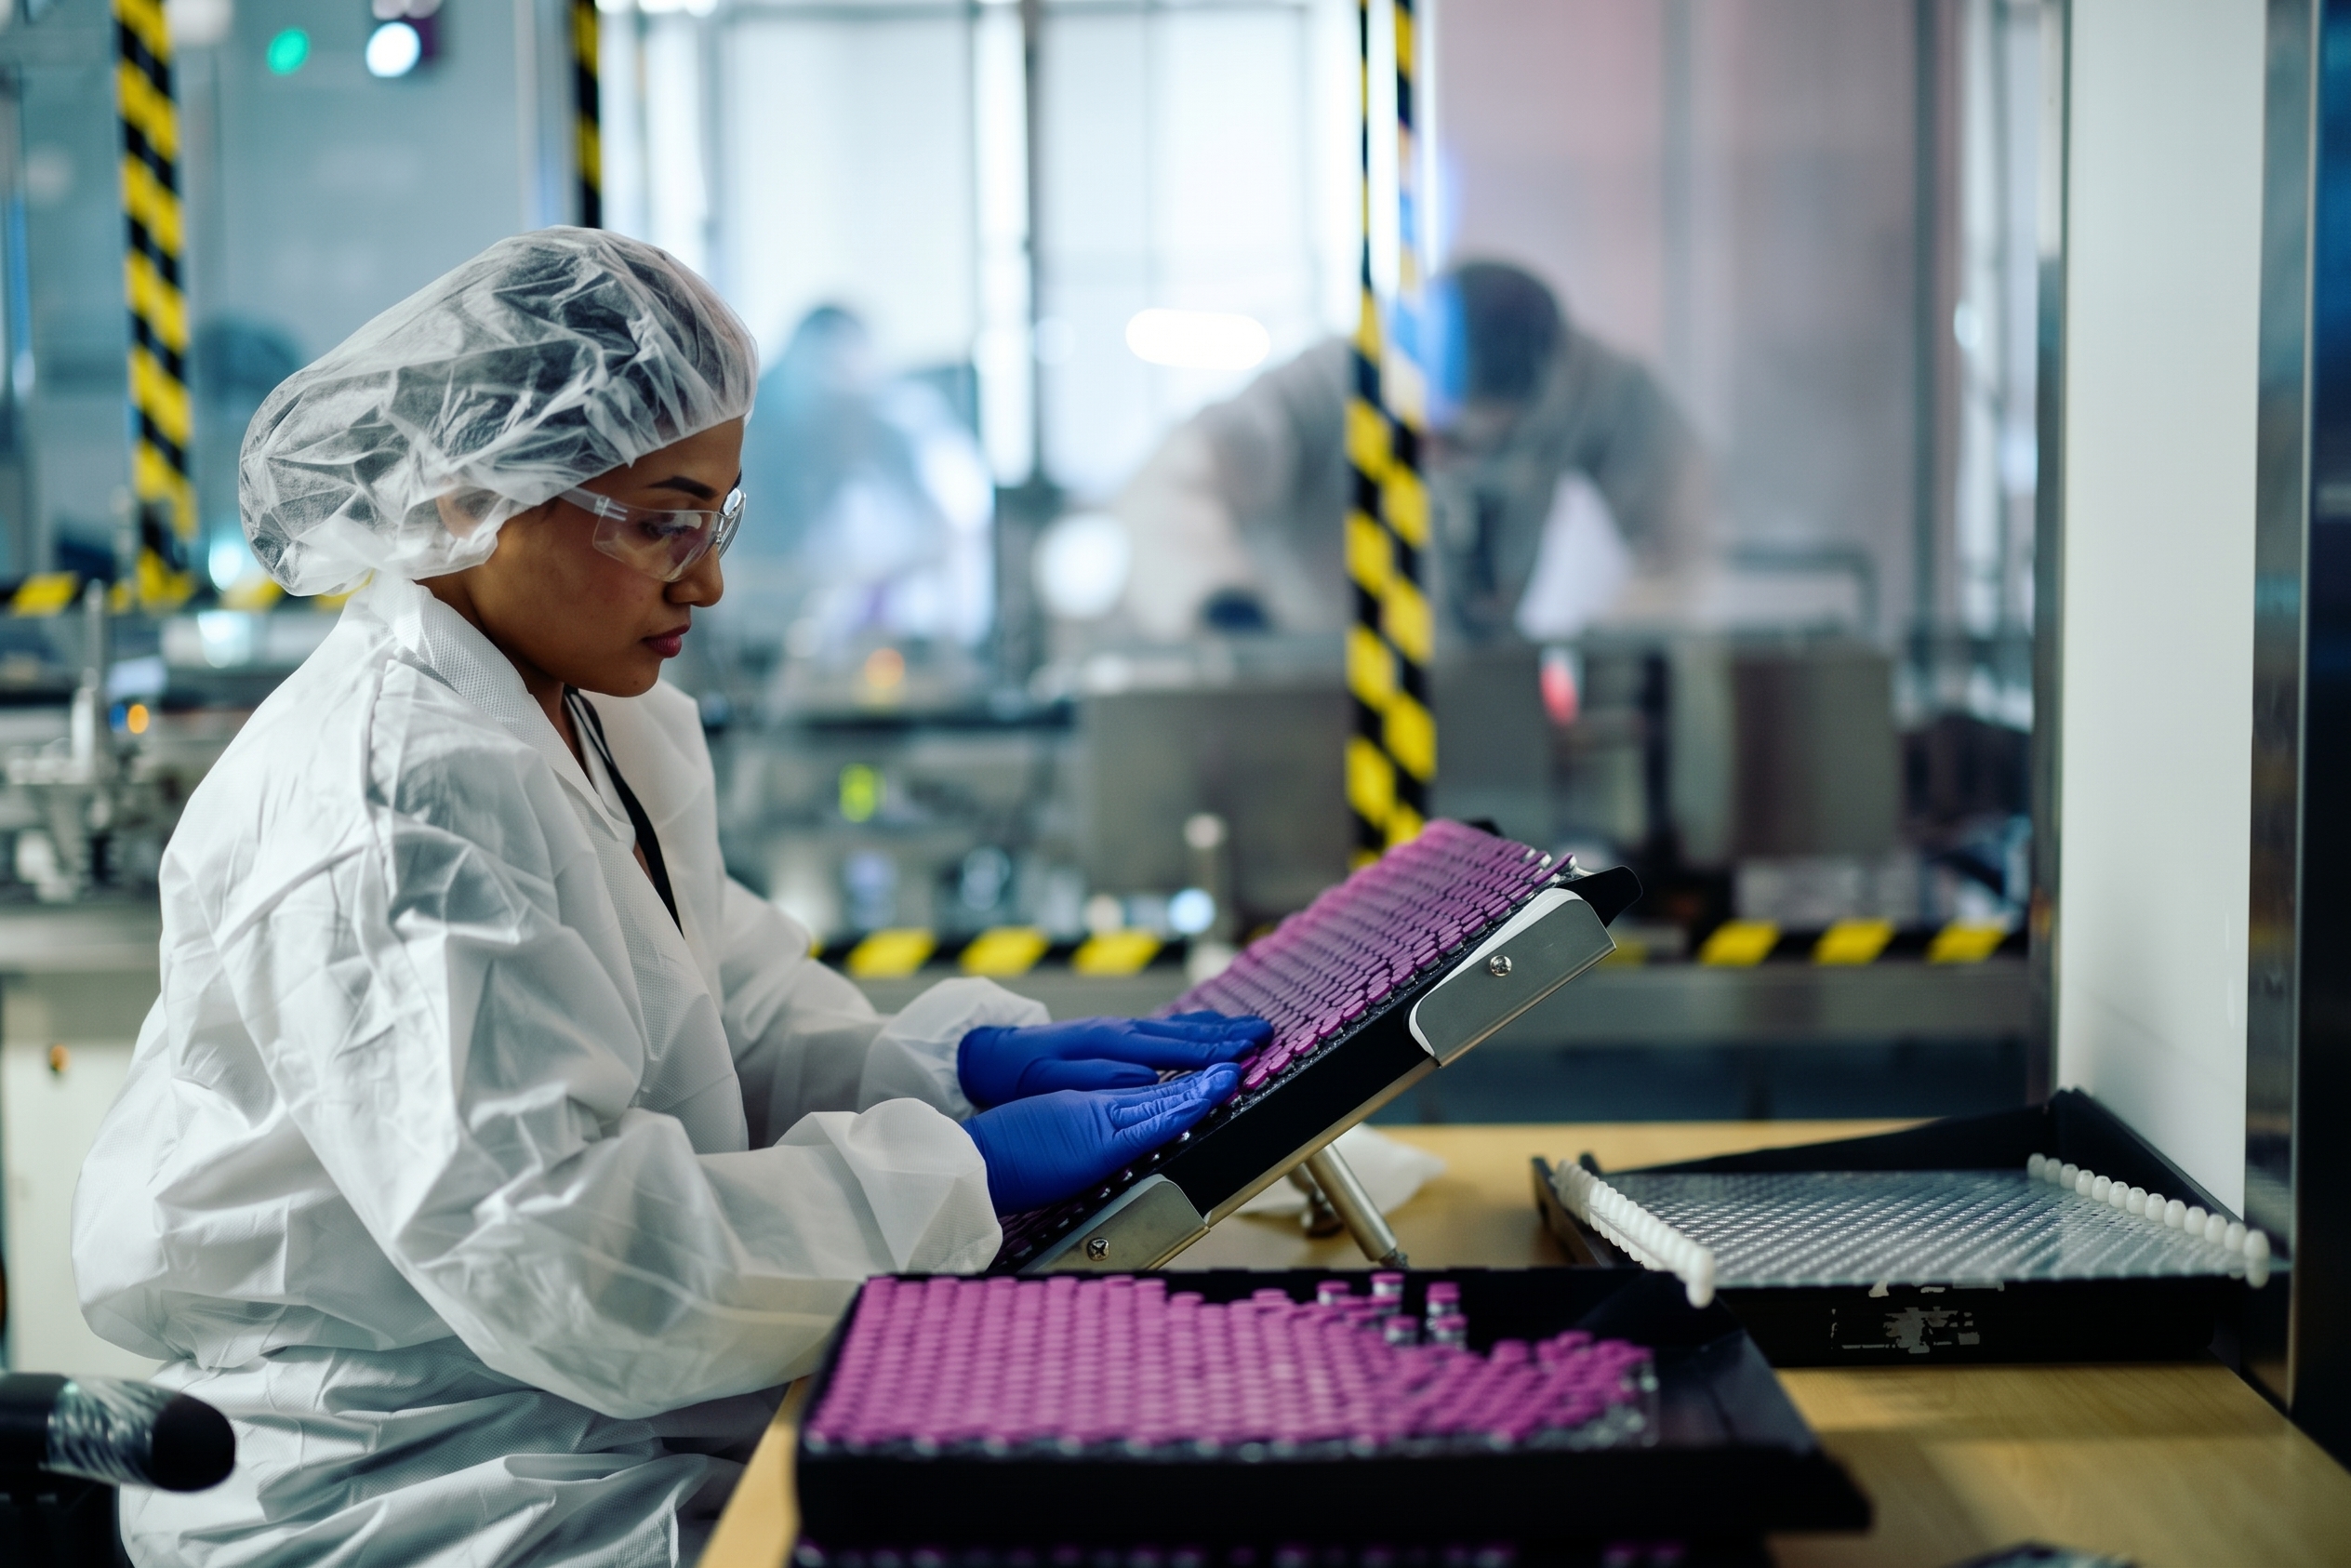
In Ohio, product goes from thaw through filling, inspection, device assembly, and final packaging, ready for distribution. Because we run our services on shared quality systems and dedicated program management, you get consistent standards whichever path you take.

Development
Process, analytical, formulation development, and process characterization, that gets your molecule clinic-ready and set up to scale.

Tech Transfer
A stage-gated transfer process with defined checkpoints, designed to get your process up and running at our sites with speed and consistency.

Biologics Drug Substance
Clinical and commercial production of monoclonal antibodies, recombinant proteins, and other complex molecules in single-use bioreactors up to 2,000L, as well as plasma proteins, transgenics, and other purification programs across a wide range of scales.

Sterile Drug Product
Formulation and aseptic filling of vials, prefilled syringes, and cartridges, from first clinical batches to commercial supply.

Device Assembly, Packaging & Logistics
Autoinjector and prefilled syringe assembly, multiple vial packaging options, plus labeling, serialization, and cold-chain logistics, all at the same site where your product is filled and inspected.
Specialized North American Operations
West Chester, Blue Ash, and Toronto each bring a defined specialty, backed by continued investment in the equipment and automation you rely on.
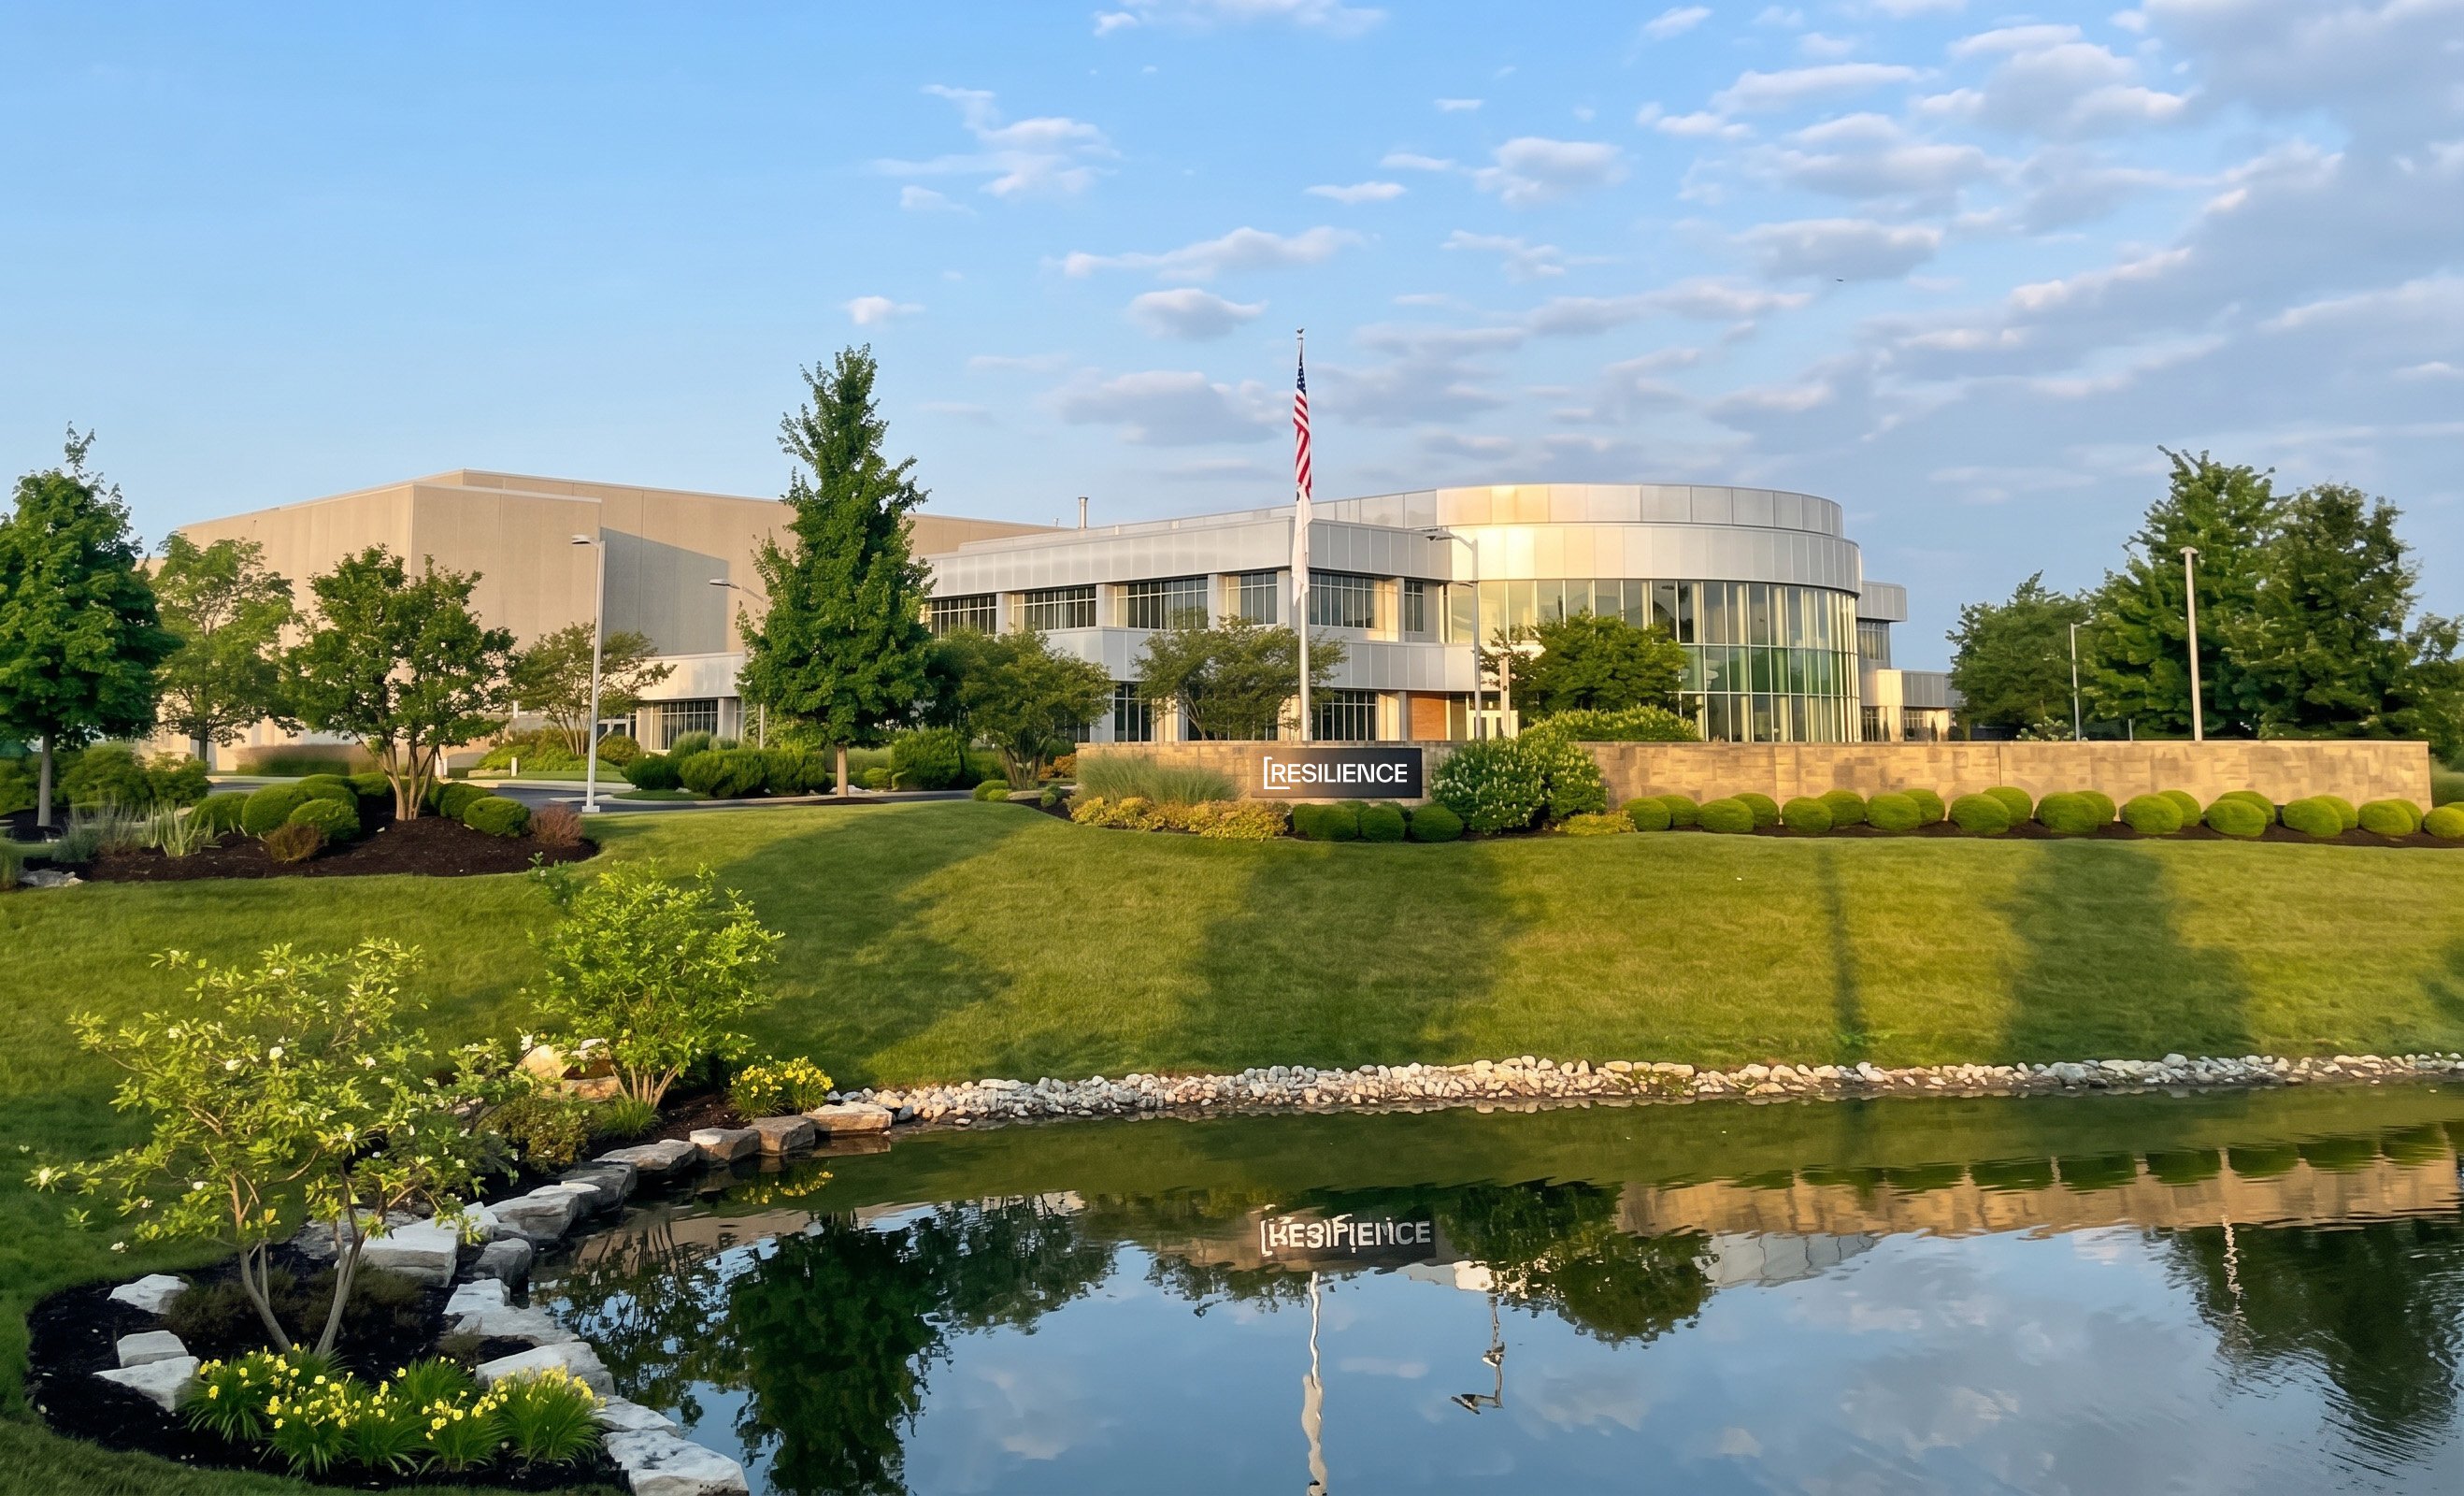
West Chester, Ohio
Greater Cincinnati, Ohio Area
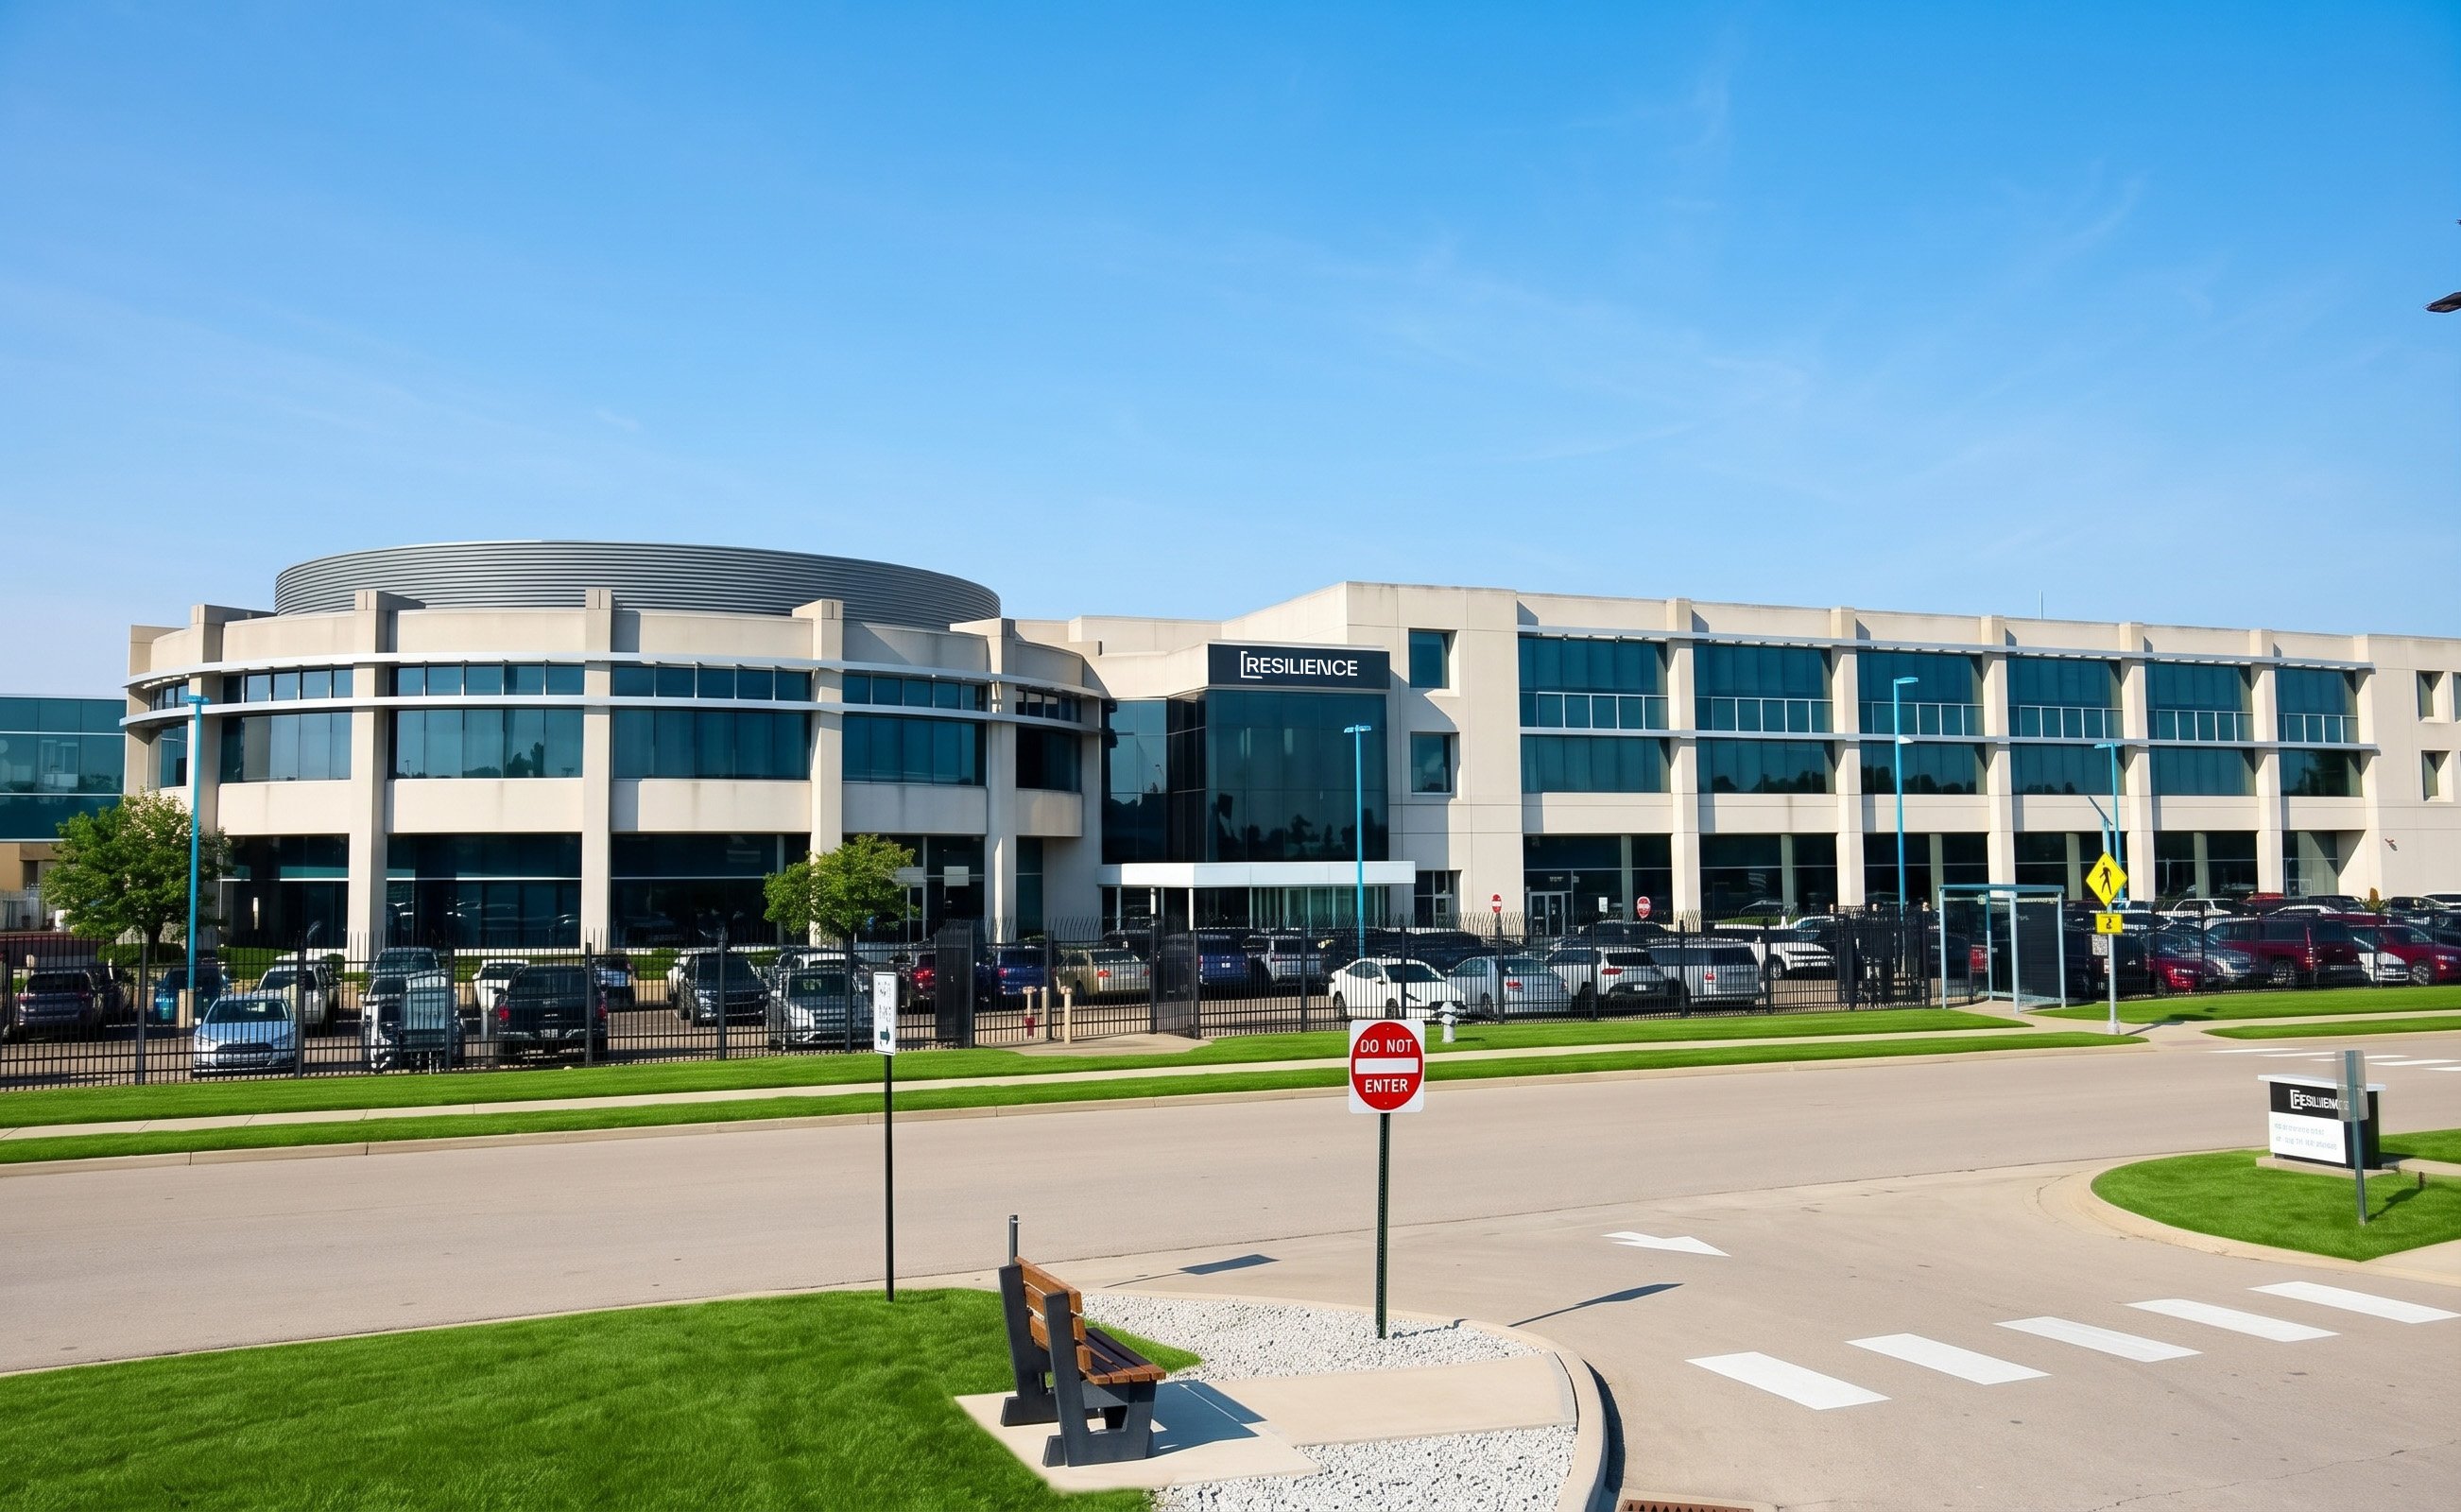
Our commercially licensed sterile drug product site spans 580,000 square feet. Teams manage everything from formulation to market-ready sterile drug product units through aseptic fill/finish manufacturing, automated visual inspection, device assembly, labeling, and packaging, enabled by digital operations and established sustainability initiatives.
Explore West Chester
Blue Ash, Ohio
Greater Cincinnati, Ohio Area
Home to our global headquarters, this 250,000-square-foot facility specializes in automated visual inspection, device assembly, labeling, packaging, cold storage, and logistics, driven by advanced equipment and dedicated operational teams.
Explore Blue Ash
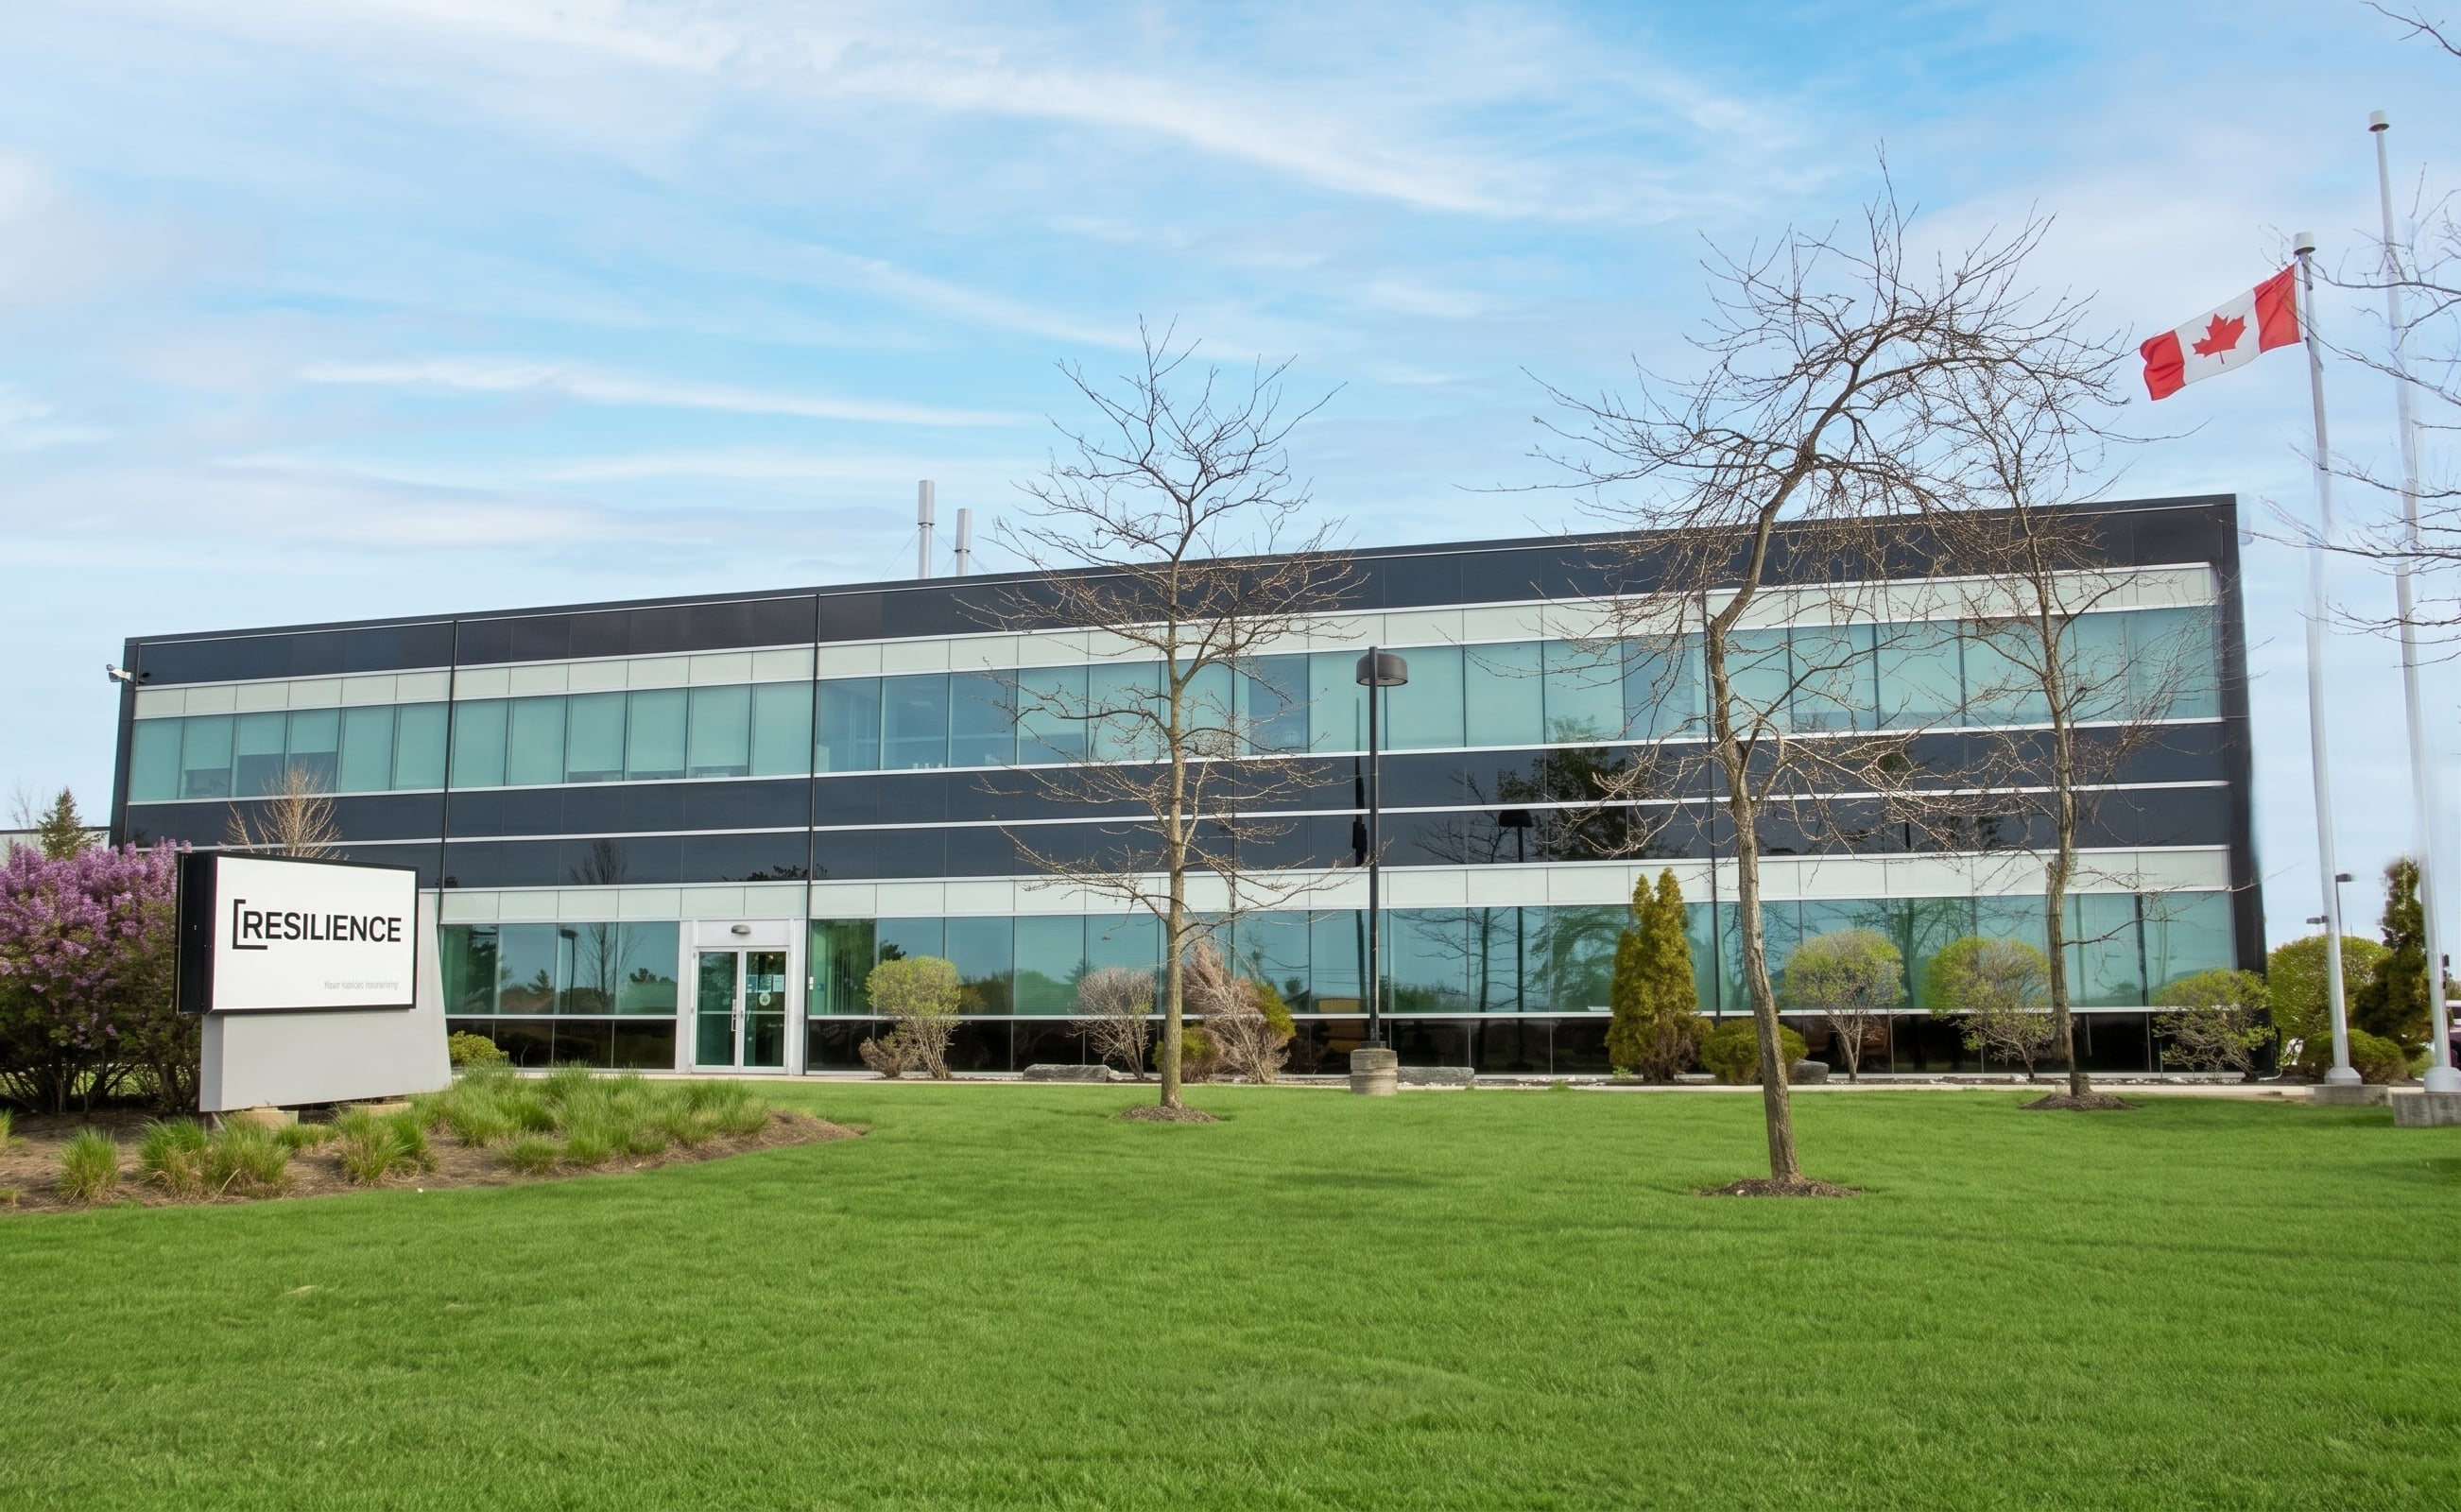
Toronto, Ontario
Canada
Our biologics hub, a 136,000-square-foot facility, drives process and analytical development, and co-localized drug substance and drug product manufacturing with additional capabilities planned. On-site capabilities include formulation, aseptic fill/finish, cold storage, and comprehensive logistics to support your clinical and commercial programs.
Explore Toronto
Let's Talk About Your Program.
Tell us your stage, timeline, and expected volumes. We'll connect you with the team who will do the work.